Hey everyone, it’s Jake here from the CNC Threading Tools team—you know, the guys you count on when your threading jobs aren’t leaving you buried in scrap parts. I get it, threading inserts can feel like a tiny, finicky nightmare when they’re not installed right, or worse, when they refuse to come out without leaving a mark on your toolholder. Last week alone, I fielded three calls from shops that ruined a $200 insert because they fumbled the swap, and two more that messed up a toolholder just yanking an old insert out wrong. So today, I’m breaking down the exact, no-BS install and removal procedures we train all our customers on—stuff that’s saved thousands of our clients from headaches (and cash) over the years. No fancy jargon, no copy-pasted supplier manuals, just what works when you’re in the middle of a tight production run. Cnc Threading Tools
First, let’s talk prep. I see so many guys skip this part because they’re in a rush to get back to the lathe, but that’s where 90% of insert issues start. When you order inserts from us, you get a little plastic case with each insert wrapped in a thin, anti-rust paper—don’t tear that off with your bare hands if you can help it, oil from your fingers will corrode the insert’s coating way faster than any coolant. Also, grab the right tools for the job: most of our toolholders come with a small torque wrench (key here is “small” — don’t use a 1/2-inch breaker bar for a T8 screw), a small wire brush, and a can of compressed air. If you don’t have those, hit our parts page and grab them—we even sell a pre-made insert swap kit for shops that do swaps daily, saves time hunting for random tools at the back of the shop.
Let’s start with removal, because sometimes you don’t have a choice—you’re mid-job and the insert chips, or it just won’t cut right, and you need it out yesterday. Wait, no—bad idea. Take 10 extra seconds to prep the toolholder first. Shut the lathe off, lock the chuck, and unplug the machine if possible. I’ve seen guys yank inserts out while the spindle’s still spinning, and let’s just say the story of the insert that flew across the shop and hit a vice is not one anyone wants to repeat. Now, locate the clamping screw—on most of our standard threading toolholders, that’s the little hex screw right in the center of the insert pocket, not the side clamp you see on some older holders. Take your hex key (or the torque driver, if you use our recommended tools) and loosen the screw, but don’t yank it all the way out yet. Here’s the trick: leave the screw loose by about 1/4 turn, then tap the top of the toolholder gently with a small brass punch or a wooden mallet. Hard metal will scratch the insert or the pocket, which makes new inserts fit loose. That tap will loosen the insert just enough that you can pull it straight out with your fingers, no prying. If the insert’s stuck (we get this all the time with chips or coolant gunk built up), don’t use a screwdriver to pry under the edge—you’ll bend the seat or crack the insert. Instead, use a compressed air can to blast the pocket out first, make sure no tiny metal shavings are in there, then try the tap method again. Worst case, send us a photo—we’ll walk you through it, no need to damage anything on your own.
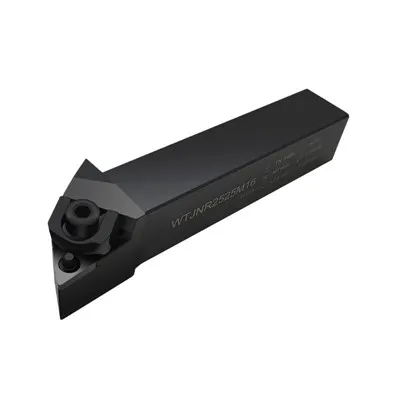
Now installation. This is where most people mess up, especially with threading inserts because the cutting edge orientation is non-negotiable. Threading is all about the angle—if the insert’s face is even 2 degrees off, you’ll get a cross-threaded part that’s scrap, and that’s money down the drain. First, clean the toolholder pocket again—even a tiny bit of old insert or coolant will make the new insert sit crooked. Use that wire brush we talked about, not a rag, because rags leave lint that gets packed in there. Now, take your new insert—look at the notches on the bottom, that’s how it aligns with the holder’s pins, so it’ll only go in one way. Don’t force it; if it doesn’t slide in smooth, you’ve got it upside down or sideways. Once it’s seated perfectly in the pocket, grab that clamping screw and thread it in by hand first. A lot of guys skip this and cross-thread the screw, which strips the holder’s thread and turns a $0.50 screw into a $150 toolholder. Hand-tighten only until it’s snug, then grab your torque wrench. Here’s the number we recommend for all our standard inserts: 8 Newton-meters. No more, no less. If you crank it too tight, you’ll crack the ceramic or carbide insert, and if you leave it too loose, it’ll shift mid-cut, leading to that cross-thread disaster I mentioned. I once had a customer who thought tighter was better, cranked a screw so hard the insert’s cutting edge chipped before he even started the first part—wasted two hours of run time before he called us. Lesson learned.
Wait, quick pro tip for left-hand vs. right-hand threading inserts: don’t mix them up. The packaging’s color-coded for you—our left-hand inserts come in blue packaging, right-hand in orange, so no more guessing. Also, if you’re doing multi-start threading, make sure the insert’s tip is aligned with the thread pitch—we list the pitch tolerance for every insert on our product pages, so you don’t have to math it out yourself.
Now, what about when inserts get worn out? A lot of guys try to reuse them, but threading inserts have a limited number of cutting edges—most of ours have 6 edges, right? Once the first edge’s dull, don’t flip it to the next one without checking the pocket again. Old edges leave tiny burrs that can scratch the new edge. We have a great video on our YouTube channel (linked on our site, just search CNC Threading Tools insert care) that walks you through flipping edges without messing up the insert.
Let’s talk common mistakes we see every day, just so you can avoid them. First, not cleaning the pocket—this is the #1 cause of loose inserts and scrap parts. Even a speck of coolant residue can make an insert sit 0.001 inch off, which is enough to throw off the thread pitch. Second, using the wrong torque—we get emails weekly from guys who used a wrench instead of the torque driver, and the screw either breaks or the insert’s too tight. Third, yanking inserts out instead of tapping—prying is the fastest way to ruin a toolholder, and replacing a toolholder is way more expensive than getting a new insert.
Now, before you go, let’s cover when you might need extra help. If you’ve tried removal and the insert still won’t budge, or if you keep breaking inserts within the first 5 parts, that’s not your fault—sometimes toolholders wear out too, or you got a bad batch. Just hit our contact button and send us your order number and a photo of the tool setup, we’ll walk you through it for free, no upselling. We’re not just a supplier—we’re machinists too, we’ve stood right where you are, covered in coolant, staring at a stack of scrap parts.
If you’ve been dealing with insert issues or want to stock up on high-quality threading inserts that fit all standard holders, don’t hesitate to reach out. We work with small shops and big factories alike, and we can get you what you need fast, with the same care we’ve used for over 10 years. No runaround, no hidden fees, just good tools and good advice.
Face Mill Cutter Heads References
- Industrial Tooling Corporation. (2022). Best Practices for CNC Threading Insert Installation and Removal. Machining Today, 18(4), 32-35.
- Kennametal. (2021). Carbide Insert Care and Maintenance Guide. Metalworking Manufacturing, 27(2), 41-44.
- Our CNC Threading Tools Internal Training Manual. (2023). Insert Swap Protocols for Standard and Custom Tooling.
- SME (Society of Manufacturing Engineers). (2020). Precision Threading in CNC Machining. SME Tech Brief, TB-20-007.
Small Craftsman (Shandong) Machine & Tools Co., Ltd.
Small Craftsman (Shandong) Machine & Tools Co., Ltd. is one of the most experienced cnc threading tools manufacturers and suppliers in China, also supports customized service with low price. Please feel free to buy bulk high quality cnc threading tools in stock here from our factory. Contact us for pricelist.
Address: No.9 Quanxin Rd., Sishui Economic Developing Zone, Jining, Shandong, China.
E-mail: 6196@ocutchina.com
WebSite: https://www.ocutooling.com/
